How Can I Tell If Pinwheel Sample Material Feel and Thickness Meet Standards?
Last month a US buyer returned a competitor’s pinwheels that felt fine but tore within weeks ISO 9073-2 for nonwovens 1. On our Zhejiang line, we judge pinwheel sample material feel and thickness differently.
Pinwheel sample material feel and thickness meet standards when micrometer readings fall inside the agreed micron tolerance on the spec sheet, the film resists tearing and fading when flexed and exposed, and the tactile hand matches a signed golden sample under identical conditions.
That answer has two halves: objective measurement and subjective feel safety certifications such as ASTM F963 2. They are separate checks, and a sample can pass one while failing the other. Let me walk you through both, step by step, the same way we run prototype evaluation in our own workshop.
What Material Thickness Range Should I Look for When Evaluating Pinwheel Samples?
Every week, buyers ask us to make blades "thicker for durability." We often push back, because on pinwheels, extra microns add weight that kills spin performance.
Look for PET or mylar blade film in the 75–150 micron range, verified with a micrometer gauge at multiple points. Thickness must sit within the tolerance band on your material specification sheet, not just feel substantial in hand.
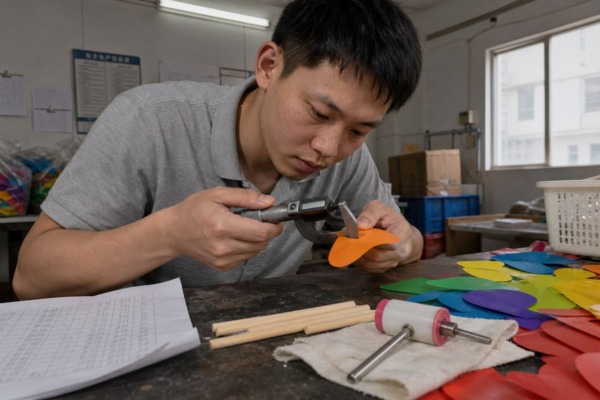
Thickness is where most sample disputes start, so I want to break it down clearly. The first rule from our production floor: always specify the exact substrate. PP, PET, and polyester film behave differently at the same micron count. A 100-micron PET blade snaps back after a fold. A 100-micron soft PP blade may stay creased. So the number alone means nothing without the material name beside it.
Typical Thickness Ranges by Component
| Component | Common Material | Typical Thickness | What to Watch |
|---|---|---|---|
| Petal blades | PET / mylar film | 75–150 microns | Too thin tears; too thick slows spin |
| Blade laminate (printed) | PP film with coating | 100–200 microns | Coating adds microns but not strength |
| Hub grommets | Molded PP plastic | 1–2 mm walls | Cracking at the pin hole |
| Dowel stick | Natural wood | 4–6 mm diameter | Consistent diameter along the shaft |
Measure Under Controlled Conditions
Compressible sheet materials change thickness depending on the pressure applied during measurement. NIST's guidance on thickness makes exactly this point: without a standardized test pressure, the reading is not comparable. That is why ASTM testing standards such as ASTM D1777 for textiles 3 and ISO 9073-2 for nonwovens define pressure, foot size, and conditioning before any reading counts. For pinwheel film, ask your supplier which method and pressure they use.
Tolerance Levels, Not Single Readings
One measurement can mislead you. We take readings at five points across each blade and compare the average and the range against the tolerance levels on the spec. A blade that averages 100 microns but swings from 80 to 120 will behave unpredictably outdoors. And remember: thicker is not automatically better. The blade's thickness-to-weight ratio drives the spin threshold, so demand micron-level numbers, not vague words like "standard gauge."
How Can I Test the Material Feel to Ensure It Won't Tear or Fade Outdoors?
During a QC round last spring, our team caught a film batch that measured perfectly but cracked at the fold line. Feel testing saved that shipment.
Test material feel by flexing each petal repeatedly, creasing an edge to check tear resistance, and running a cross-hatch tape test (ASTM D3359) on printed areas. Combine this with UV exposure checks to confirm colors will not fade outdoors.
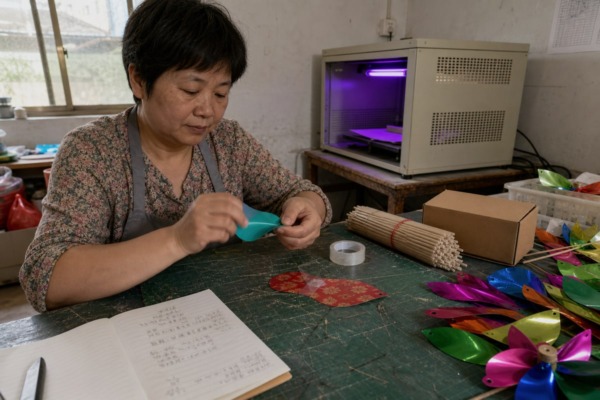
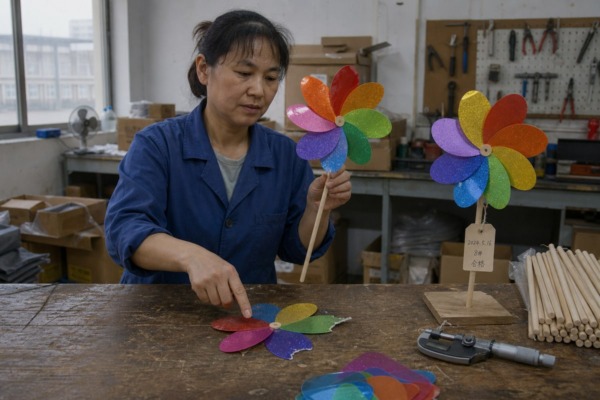
Some buyers tell me feel is too subjective to belong in a standards discussion. I understand that objection, and in pure engineering contexts it holds. But pinwheels are consumer products, often for children's gardens, and tactile properties shape perceived value more than a ten-micron difference ever will. The practical answer is to translate feel into repeatable checks. Here is the hand-test routine I use on every incoming sample, the same one I run when comparing against our retained standard sample:
- Touch the film thickness and toughness. Pinch each petal between thumb and forefinger. Flex it against the standard sample. Note any difference in stiffness, snap-back, or surface texture.
- Crease and release. Fold a blade edge sharply, then release. Good PET film shows a light line but no whitening or splitting. Whitening signals brittleness that becomes tearing outdoors.
- Check the dowel hardness. Press a fingernail into the wooden stick. Compare the hardness against the master sample. A soft, punky dowel snaps in wind.
- Record every difference. We log hand-feel and thickness deviations in writing, sample by sample. Memory fades; records do not.
Turning Feel into Numbers
Where you need objectivity, borrow measurable proxies. Shore Durometer testing quantifies stick or hub hardness with a repeatable number. The fabric hand concept from textiles applies here too: softness, drape, and surface roughness can all be scored. For outdoor life, ask about Environmental Stress Cracking Resistance (ESCR) testing, which checks whether the film thickness survives combined UV and mechanical stress. A blade that passes ESCR will not turn brittle after one summer in direct sun.
What Quality Control Checks Should I Request Before Approving a Bulk Pinwheel Order?
A procurement manager from Texas once messaged me on WhatsApp: "Your sample passed. How do I know the container will?" Great question, and it deserves a clear checklist.
Request a signed golden sample, a material specification sheet listing substrate and micron tolerance, safety certifications such as ASTM F963 or EN71, cross-hatch adhesion results, edge-profile inspection, and a spin test on assembled units before approving any bulk pinwheel order.
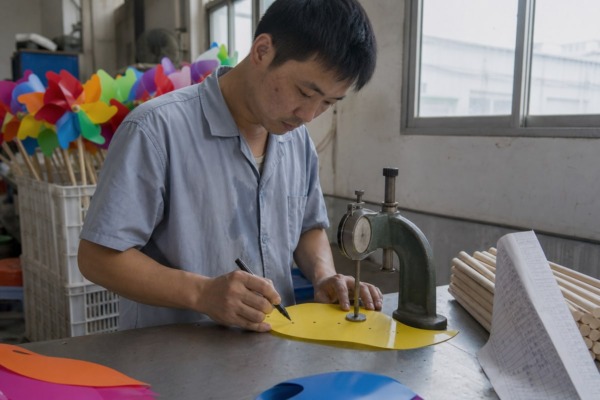
Sample approval is a contract moment, not a formality. On our line, we treat the approved sample as the legal reference for everything that follows. The single most powerful tool here is the Golden Sample protocol: one physical unit, signed and dated by both sides, kept by both sides. When a dispute comes up six months later, nobody argues about descriptions. We compare against the object.
The Pre-Approval QC Checklist
| Check | What It Verifies | How It Is Done |
|---|---|---|
| Golden sample sign-off | Master reference for feel and thickness | Signed physical unit retained by buyer and factory |
| Material specification sheet | Substrate type, micron thickness, tolerance band | Documented spec with GSM measurement for any fabric parts |
| Safety certification | Toxicity and physical safety compliance | ASTM F963 or EN71 test reports for children's products |
| Print adhesion | Coating will not peel when flexed | Cross-hatch tape test per ASTM D3359 |
| Edge-profile inspection | No burrs harming tactile safety | High-magnification check of die-cut petal edges |
| Spin test | Thickness-to-weight ratio meets performance | Assembled unit tested for rotational efficiency |
Why Documentation Beats Trust
Quality assurance testing only protects you if the results are written down before production starts. I always advise buyers to request the full material data sheet, not a one-line description. For the US and European markets we ship to, ASTM F963 and EN71 documentation is non-negotiable because pinwheels are handled by children. The edge-profile inspection matters more than people expect: microscopic burrs on die-cut petals ruin the hand of the product and can scratch small fingers. Ten minutes under magnification during prototype evaluation prevents an entire container of returns.
How Do I Compare Sample Consistency Across Multiple Production Batches From My Supplier?
I learned this lesson the hard way early in our export business: two batches can pass individually yet feel completely different side by side. Consistency needs its own system.
Compare batches by measuring thickness at the same points with the same micrometer gauge, touching film toughness and stick hardness against a retained golden sample, and recording every feel or thickness difference in a batch log for trend tracking.
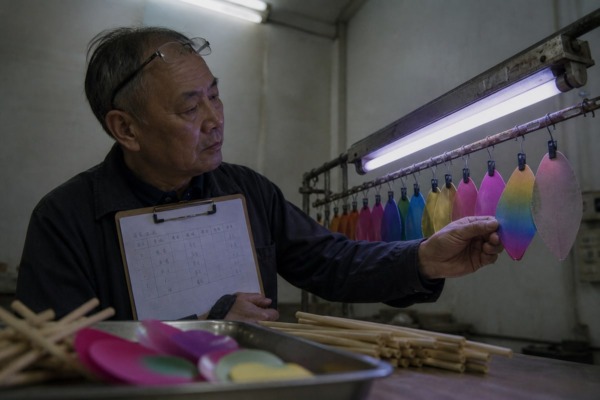
Batch drift is quiet. No single delivery fails outright, but resin lots change, print coatings vary, and wood dowels come from different mills. By batch five, the product no longer matches what your customers bought in batch one. The fix is a disciplined comparison routine, and it is exactly what we run internally before every shipment: pull units from the new batch, place them next to the standard sample, touch the film thickness and toughness, test the rod hardness, and write down the differences in hand feel and thickness. Nothing goes to packing until the log is clean.
A Simple Batch Comparison Log
| Log Field | Batch 1 Baseline | New Batch Reading | Action Trigger |
|---|---|---|---|
| Blade thickness (5-point avg) | Per spec sheet | Measured same points, same gauge | Outside tolerance band |
| Hand feel vs golden sample | Match | Stiffer / softer / rougher noted | Any repeated deviation |
| Dowel hardness | Baseline durometer score | New durometer score | Softer than baseline |
| Color and print | Match | Fade or hue shift noted | Visible difference |
| Spin performance | Baseline spin threshold | Same test conditions | Slower start-up |
Keep the Method Constant
Consistency comparisons only work if the method never changes. Use the same micrometer gauge, the same measurement points, and the same conditioning time before readings, because humidity and temperature affect dimensional stability in both film and wood. For assembled units where a contact gauge cannot reach, non-destructive ultrasonic gauging under ISO 16809 4 verifies thickness on curved blades without damaging the piece. And do not settle for one number per batch. Track the average and the range together, so you catch widening variation before it becomes a customer complaint.
Conclusion
Feel screens; measurement confirms. Verify micron tolerance with the right ASTM or ISO method, judge hand against a signed golden sample, and log every batch difference.
Footnotes
1. International standard for determining the thickness of nonwoven textiles. ↩︎
2. Mandatory safety standard for all toys sold in the United States. ↩︎
3. Updated to the current 2026 revision of the ASTM D1777 standard, replacing the 404 link. ↩︎
4. Standard for non-destructive ultrasonic measurement of material thickness. ↩︎
More Articles
You might also find these helpful.
How to Remotely Verify a Factory's Production Capabilities for Wrought Iron Plug-In Components?
Verify pinwheel sample material feel and thickness meet standards with micron checks, tear-flex tests, and golden-sample comparisons before…
Read More →
How to Assess a Factory's Production Capacity When Sourcing Wrought Iron Inserts?
Verify pinwheel sample material feel and thickness meet standards with micron checks, tear-flex tests, and golden-sample comparisons before…
Read More →
What Questions Should You Ask Wrought Iron Insert Suppliers to Spot Unreliable Ones Early?
Verify pinwheel sample material feel and thickness meet standards with micron checks, tear-flex tests, and golden-sample comparisons before…
Read More → English
 Spanish
 German
 Arabic