How to Request Pre-Shipment Quality Inspection Reports for Windmill Suppliers?
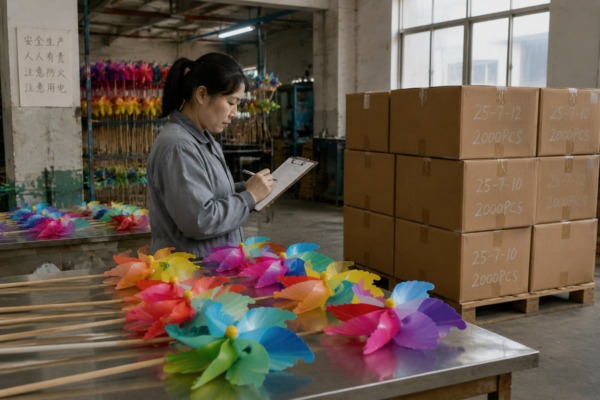
A buyer once received faded, bent windmills with no pre-shipment quality inspection report 1 to lean on. On our pinwheel production line, that report is non-negotiable.
Request pre-shipment quality inspection reports for windmill suppliers by writing them into your purchase order as a mandatory deliverable. Specify appearance, dimensional, and safety checks, AQL sampling, photo evidence, and a clear pass/fail verdict, then confirm the full report before releasing bulk shipment.
That is the short answer. The rest of this guide breaks it down step by step. I will show you what to put in the request, how to verify the report, when to schedule the inspection, and what to do when a supplier stalls. Everything here comes from real export work, not theory.
What Details Should I Include When Requesting a Pre-Shipment Inspection Report From My Windmill Supplier?
Last month, a US procurement manager messaged us on WhatsApp: "Your quote looks great — but what exactly should my inspection request say?" Her question deserved a precise answer.
Include the product model and PO number, lot and shipment quantity, AQL sampling level, a visual inspection checklist, dimensional verification tolerances, safety test requirements, packaging and marking checks, photo evidence, the inspector's name and signature, and a clear pass, fail, or hold verdict.
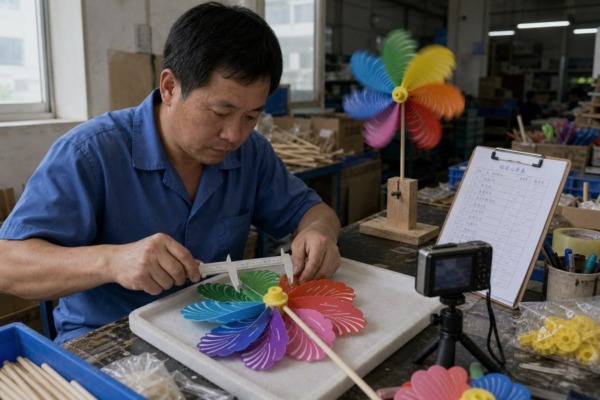
The biggest mistake I see buyers make is asking for "a QC report" with no scope. That request produces a one-page certificate with a stamp. It proves nothing. A useful request defines the report before production even starts.
The Core Checklist: Appearance, Dimensions, Safety
In our own export practice, we tell every buyer the same thing: require a complete quality inspection report before shipment, covering appearance, dimensions, and safety testing, and confirm that report before the bulk goods leave the factory. For decorative windmills and pinwheels, appearance means color accuracy, print alignment, and surface coating inspection for UV fade resistance. Dimensions mean petal spread, stick length, and hub fit. Safety means spin function, pin security, sharp-edge checks, and small-parts risks for children's markets.
Here is the full set of elements your request should name:
| Report Element | What to Specify | Why It Matters |
|---|---|---|
| Order details | Model, PO number, lot size, shipment quantity, inspection date and location | Ties the report to your exact goods |
| Sampling plan | AQL level and general inspection level | Makes pass/fail objective, not opinion |
| Visual inspection checklist | Color, print, scratches, coating defects | Catches appearance issues item by item |
| Dimensional verification | Key measurements with tolerances | Confirms parts fit and match the golden sample |
| Safety testing | Spin test, pin pull, edge check | Protects end users and your liability |
| Packaging and marking | Carton strength, labels, shipping marks | Prevents transit damage and customs delays |
| Photo evidence | Wide shots plus defect close-ups | Turns claims into proof |
| Verdict and signature | Pass, fail, or hold, with inspector identity and date | Supports acceptance and dispute resolution |
Scaling the Request: Decorative Windmills vs. Utility-Scale Turbines
If you source industrial wind equipment instead of garden decorations, the same logic scales up. Buyers of large turbines should reference IEC 61400 compliance 2 in the PO, demand non-destructive testing (NDT) records for structural welds against an approved welding procedure specification, and require a Material Traceability Report plus component certification documents for blades, hubs, and fasteners. The structure of the request is identical. Only the technical depth changes.
How Can I Verify That My Supplier's Quality Inspection Report Is Accurate and Trustworthy?
Early in our export years, we watched a competitor's "passed" report unravel under scrutiny — recycled photos, no sampling math. That episode shaped how our own Quality Assurance documentation is built today.
Verify a windmill supplier's inspection report by cross-checking photos against your golden sample, confirming the sampling math matches the stated AQL, checking inspector identity and dates, requesting raw measurement data, and commissioning a third-party inspection agency to re-inspect a random portion of the lot.
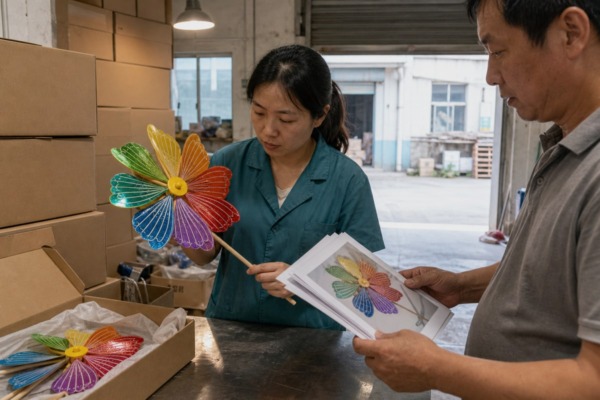
Trust is not a feeling in procurement. It is a process. A report can look polished and still hide problems, so you need a repeatable way to test it.
Six Checks Before You Trust Any Report
First, check the photos. They should show your actual product, your carton marks, and this production date — not stock images from a previous run. Second, do the sampling math. If the lot is 10,000 windmill sets and the report claims 20 pieces were checked, that does not match any standard AQL general inspection 3 level. Third, look for defect records. A report with zero minor defects across thousands of hand-assembled pinwheel petals is a red flag, not a green one. Real production always shows some minor findings. Fourth, confirm the inspector's name, signature, and date. Fifth, ask for raw data behind the dimensional verification, not just "OK" marks. Sixth, spot-check independently when the order value justifies it.
Supplier-Issued vs. Third-Party Reports
| Factor | Supplier's Internal QC Report | Third-Party Inspection Agency Report |
|---|---|---|
| Cost | Usually free | Inspection fee per man-day |
| Speed | Fast, no scheduling friction | Needs booking and factory access |
| Objectivity | Depends on supplier culture | Independent by design |
| Best use | Repeat orders with trusted partners | New suppliers, high-value or custom lots |
| Evidence standard | Varies widely | Templated, photo-rich, checklist-driven |
Some suppliers push back on detailed reporting, seeing it as distrust of their internal QA. I understand the feeling, but I reject the conclusion. When our factory documents a lot properly, disputes drop for both sides. Digital, templated QC reporting is now the trend precisely because it protects everyone, and it makes packaging, labeling, and defect evidence easy to capture in one standard format.
When Is the Best Time in Production to Schedule My Pre-Shipment Quality Inspection?
Every season, we weigh the same trade-off at our Zhejiang factory: inspect too early and the sample lies; inspect too late and the container is already booked.
Schedule the pre-shipment quality inspection when production is 100% complete and at least 80% of goods are packed, before container loading. This timing lets inspectors sample the true bulk lot while leaving room for rework, re-inspection, and corrective action before dispatch.
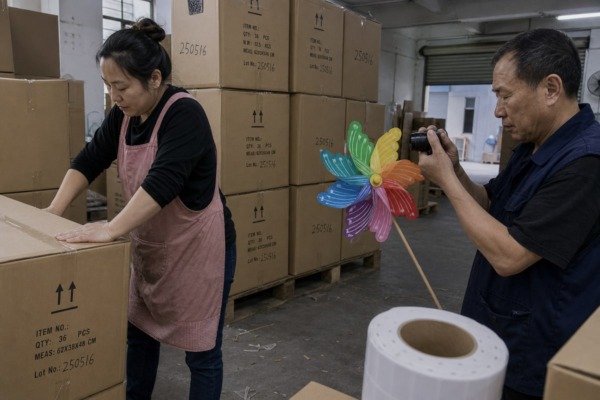
Timing decides whether an inspection is useful or just ceremonial. If you inspect at 50% production, the sample may not represent the final lot. If you inspect after the container doors close, a failed result costs you unloading fees and missed vessel bookings.
Comparing Your Timing Options
| Inspection Window | Production Stage | Strength | Weakness |
|---|---|---|---|
| During-production check | Roughly 20–80% complete | Catches systemic issues early | Cannot judge the finished lot |
| Pre-shipment inspection | 100% produced, 80%+ packed | Samples the real shipping lot | Rework window is short |
| Loading supervision | At container stuffing | Verifies quantity and handling | Too late to fix product defects |
For our pinwheel and windmill strings orders, the pre-shipment window is the anchor. It confirms the goods as they will actually ship — petals assembled, grommets seated, sticks packed, cartons marked. Then we confirm the full report with the buyer before bulk release. That confirmation step is the habit I push hardest.
Build In Buffer Days
Inspection reports typically arrive within a few working days after the site visit. Plan for that. I advise buyers to leave five to seven days between inspection and vessel cutoff. That buffer covers report review, punch list clearance for any minor findings, and a re-inspection if something fails. For industrial turbine buyers, this window also aligns with Factory Acceptance Test (FAT) completion — covering blade pitch functionality, generator efficiency, and gearbox vibration — so dispatch approval rests on tested performance, not on schedule pressure.
What Should I Do If My Windmill Supplier Delays or Refuses to Provide an Inspection Report?
During one peak season, a fellow exporter stalled on a buyer's report request for two weeks. Our team watched that order collapse — and learned what buyers should do instead.
If your windmill supplier delays or refuses an inspection report, restate the contractual requirement in writing, hold the balance payment, offer a third-party inspection agency at your cost as an alternative, set a firm deadline, and pause the shipment release until documentation arrives.
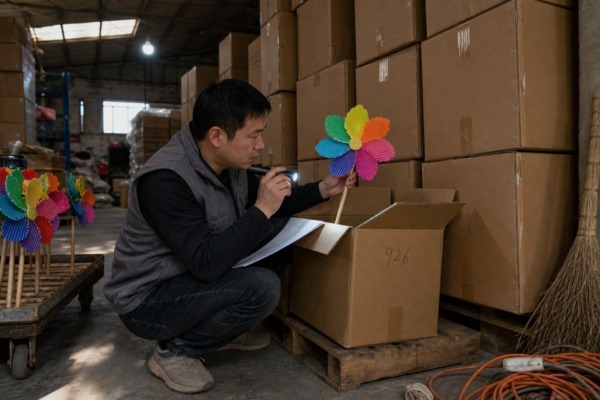
A delay is not always deception. Sometimes it is peak-season chaos or weak documentation habits. But your response should be structured either way, because pre-shipment quality inspection reports for windmill suppliers only protect you if they arrive before the goods do.
The Escalation Path, Step by Step
- Restate the requirement in writing. Quote the PO clause that names the report as a mandatory pre-shipment deliverable. Written records matter if the dispute grows.
- Ask why, specifically. Is production behind? Is the QC team stretched? A real reason has a real date attached.
- Set a firm deadline. Give a short, clear window. Vague patience trains suppliers to deprioritize you.
- Offer the third-party option. Propose an independent inspector at your cost, with factory access to the production lot and packing area. A cooperative supplier accepts. A refusal here is the strongest warning sign you will get.
- Hold the balance payment. Tie final payment to report approval. This is standard leverage, not hostility, and our factory works under such terms without complaint.
- Pause the release and score the supplier. No approved report, no shipment. Then log the incident in your supplier scorecard for future sourcing decisions.
Some sellers argue that minimal documentation speeds delivery. I hear this often, and for a distributor facing shipping delays 4 it sounds tempting. But the math rarely works. The cost of one inspection is small next to the cost of returns, damaged packaging claims, and rework logistics after a bad container lands. Verification beats speed every time the product carries your brand.
Conclusion
Skipping inspection reports invites hidden defects, returns, and disputes. Specify the report early, demand evidence, verify it, time it right — and never release a windmill shipment without it.
Footnotes
1. ASQ provides authoritative resources on quality assurance documentation and the standards for professional quality inspection reporting. ↩︎
2. The IEC 61400 series provides international standards for the design, safety, and testing of wind turbine systems. ↩︎
3. ISO 2859-1 is the international standard for sampling procedures and general inspection levels used in AQL-based quality control. ↩︎
4. The International Trade Administration offers guidance for businesses managing international logistics and mitigating common shipping delays. ↩︎
More Articles
You might also find these helpful.
How to Remotely Verify a Factory's Production Capabilities for Wrought Iron Plug-In Components?
Get concrete requirements for pre-shipment quality inspection reports from windmill suppliers, from AQL sampling to photo evidence, before…
Read More →
How to Assess a Factory's Production Capacity When Sourcing Wrought Iron Inserts?
Get concrete requirements for pre-shipment quality inspection reports from windmill suppliers, from AQL sampling to photo evidence, before…
Read More →
What Questions Should You Ask Wrought Iron Insert Suppliers to Spot Unreliable Ones Early?
Get concrete requirements for pre-shipment quality inspection reports from windmill suppliers, from AQL sampling to photo evidence, before…
Read More → English
 Spanish
 German
 Arabic